 KELIBRON
Measuring methods
Measuring a bore with a dial bore gauge
A dial bore gauge measures a bore by comparison: set it to the nominal size on a ring gauge (or a gauge-block stack), rock it gently in the bore, and read the minimum at the turning point. Bore size = setting size + reading — a plus reading means the bore is larger than the setting.
On this page
What it is
A dial bore gauge is a two-point contact instrument for bores: a dial indicator on top, an interchangeable measuring head below, and a self-centering bridge that keeps the measuring line through the bore centre. It reads differences, not absolute sizes, so it always needs a reference of known size.
In China the product family is covered by GB/T 8122-2024 (current); the standard has carried the name 内径指示表 since the 2004 edition — the 1987 edition was titled 内径百分表, the name shops still use. It is not an inside micrometer: the contact is two-point with a centering bridge, and the size comes from the setting plus the reading.
Setting the gauge to size
The gauge is zeroed on a reference of the nominal size. Three references are in common use (textbook: 金莹, 公差配合与技术测量): a master ring gauge — accurate and the easiest, which is why shops that check the same bore in batches keep one; a gauge-block stack clamped between the measuring faces — accurate but fiddly; and an outside micrometer set to the size — convenient, but the setting inherits the micrometer’s own error.
When mounting the dial, pre-compress it before locking it — enough that the reading can swing either side of zero. Hold the gauge by its insulated handle during both zeroing and measuring, not by the metal.
Measuring: rock, and read the minimum
Tilt the head to slip it into the bore, then straighten it. Rock the gauge gently in the axial plane — the plane through the bore axis. Away from the true diameter the two contacts span a chord, which reads larger; at the turning point of the swing the span is the diameter itself, and that is where the pointer stops and comes back. Read the minimum at that point.
The sign matters: reading = actual bore − setting size. A reading on the plus side means the bore is larger than the reference. A reading taken before the turning point, or with the gauge still tilted along the bore, is a chord or a diagonal, not the diameter.
A worked example
The setting ring is Ø28.00 mm and the bushing bore is specified Ø28 +0.05/0. Set to zero on the ring, rock in the bore, and read +0.030 mm at the turning point: bore size = 28.00 + 0.030 = 28.030 mm — inside 28.00 to 28.05, so the bore passes.
| Item | Value |
|---|---|
| Setting size (ring gauge) | 28.00 mm |
| Reading at turning point | +0.030 mm |
| Bore size | 28.030 mm |
| Tolerance Ø28 +0.05/0 | 28.00–28.05 mm, pass |
Practice points
Measure in at least two directions 90° apart and at more than one depth; the spread between readings shows out-of-round and taper (see measuring a bore). Clean the bore first — a chip under a contact point reads as a local diameter change.
For loose tolerances a caliper is faster; choose by the tolerance. The dial bore gauge earns its place when the tolerance is tighter than a caliper can judge repeatably, or the bore is deep and a caliper cannot be rocked properly.
Standards
The product standard is GB/T 8122-2024 (current), which replaced GB/T 8122-2004. Verification of the dial indicator on top follows JJG 34-2022 (current), which replaced JJG 34-2008 and JJG 379-2009.
Planned for the lab
Dial bore gauges are planned for KELIBRON (intake group G2). The Ø28 bushing bore already in the lab will be the first workpiece; its Ø28 setting ring (or a gauge-block stack) arrives with the same intake. Until then, practise the rock-for-the-extreme reading on the caliper bore scene below — the geometry error it teaches is the same one the bore gauge avoids.
References
- GB/T 8122-2024《内径指示表》 · 国家市场监督管理总局、国家标准化管理委员会
- JJG 34-2022《指示表检定规程》 (cited by number; no public page) · 国家市场监督管理总局
- 金莹 主编,《公差配合与技术测量》,清华大学出版社,2014(2024 年第 4 次印刷),ISBN 978-7-302-37145-8 (cited by number; no public page) · 清华大学出版社
How the guides are checked against these sources: About KELIBRON.
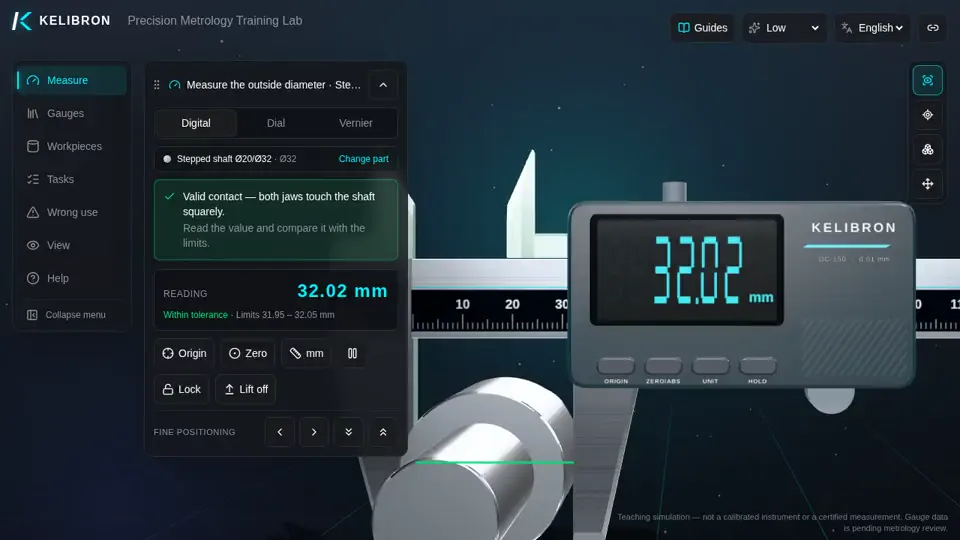
Practise the shared basics on a caliper
Questions
How do I set a dial bore gauge to size?
Zero it on a reference of the nominal size: a master ring gauge is the most accurate and convenient, a clamped gauge-block stack is accurate but fiddly, and an outside micrometer is convenient but passes its own error into the setting.
Do I read the maximum or the minimum while rocking?
The minimum, at the turning point of the swing. Off the true diameter the contacts span a chord, which reads larger; the pointer reverses exactly where the span is the diameter.
How do I work out the bore size from the reading?
Bore size = setting size + signed reading. A plus reading means the bore is larger than the setting, a minus reading smaller — record the sign every time.
Practise the basics first
Cleaning, zero checks, square positioning, light even force and reading to the scale interval are the same on every instrument; practise them in a caliper scene.
Related guides
 Measuring methodsHow to measure a machined partWork from the drawing, one feature at a time: what is the feature and its tolerance, which instrument has an error of about a tenth of that tolerance, how to hold the part and the instrument, where and how many times to measure, and how to record the result.
- Measuring methodsMeasuring common partsMeasure every diameter at several places along the part and in two directions 90° apart; the spread reveals taper and out-of-round.
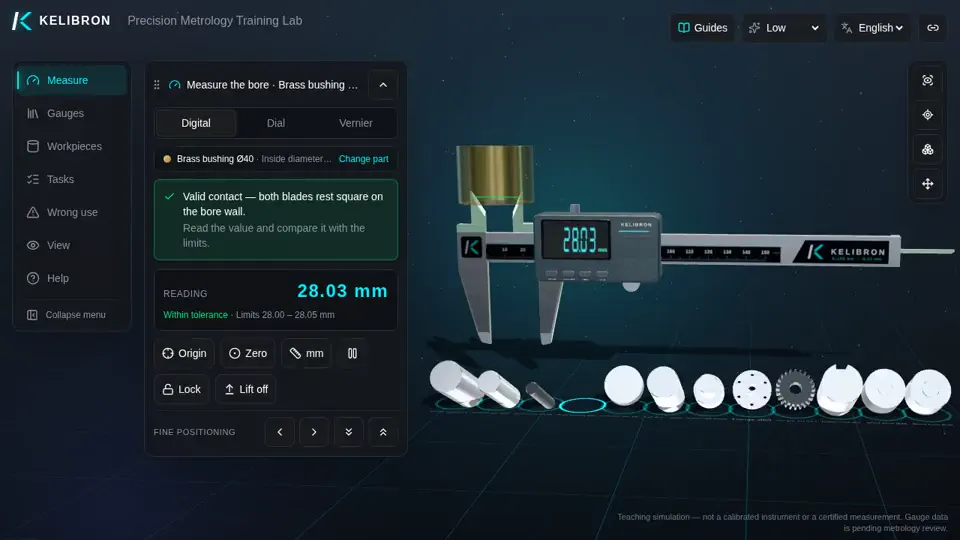 Measuring methodsHow to Measure a BoreTo measure a bore with a caliper, put the inside jaws well into the hole, across the centre, and rock them gently for the largest reading; then repeat at 90°.