 KELIBRON
Tolerances and decisions
General tolerances for untoleranced sizes
A size with no tolerance next to it takes the general tolerance named on the drawing, for example “GB/T 1804-m”. Look up the class and the size range in the table: in GB/T 1804-2000, class m allows ±0.2 mm from over 6 mm up to 30 mm and ±0.3 mm from over 30 mm up to 120 mm. Unless otherwise specified, a part outside a general tolerance should not normally be rejected if its function is not impaired.
On this page
- What is a general tolerance?
- Where the drawing says which class applies
- Reading the table for linear sizes
- How to look up a size: worked examples
- Radii, chamfers and angles
- When a size gets its own tolerance
- Judging a size against a general tolerance
- Practising in KELIBRON
- References
- Watch it done
- Practise in the lab
- Questions
What is a general tolerance?
GB/T 1804-2000 defines general tolerances as the tolerances that can be held under the usual conditions of a workshop. A size that takes the general tolerance carries no limit deviations of its own. The standard covers linear sizes (outside, inside and step sizes, diameters, radii, distances, outside radii and chamfer heights), angles, including right angles that are usually not dimensioned, and the sizes of machined assemblies. It applies to sizes made by cutting metal and by ordinary pressing; other materials and processes may refer to it.
Angles covered by GB/T 1184 and the angles of regular polygons are excluded. It does not apply to auxiliary sizes in brackets, to theoretically exact sizes in a frame, or to sizes covered by another general tolerance standard.
Where the drawing says which class applies
GB/T 1804-2000 has four classes: f (fine), m (medium), c (coarse) and v (very coarse). The drawing names the standard and the class near the title block, in the technical requirements or in a referenced document such as a company standard (clause 6). For class m the note reads GB/T 1804-m. How to read the other sizes on a drawing is covered in reading sizes on a drawing.
GB/T 1804-2000 is an equivalent adoption (eqv) of ISO 2768-1:1989, so a drawing to the international standard says ISO 2768-m. If your drawing cites ISO 2768, look up its own table; this article quotes the Chinese standard.
Reading the table for linear sizes
GB/T 1804-2000 Table 1 lists the permitted deviations for linear sizes, in millimetres, with one row per class and one column per size range, from 0.5–3 mm up to over 2000 to 4000 mm. Each range includes its upper value: “over 6 to 30” includes 30 mm. The finer the class and the smaller the size, the smaller the deviation. Take the values from the standard itself; the two used in the examples below are class m, over 6 to 30 mm: ±0.2 mm, and class m, over 30 to 120 mm: ±0.3 mm.
How to look up a size: worked examples
- Find the class in the general tolerance note.
- Find the range that contains the nominal size.
- Read the deviation and add it to the nominal size on both sides.
With the note GB/T 1804-m: a length of 50 mm lies in “over 30 to 120”, so it may be 50 ± 0.3, that is 49.7 to 50.3 mm. A diameter of 12 mm lies in “over 6 to 30”: 12 ± 0.2, that is 11.8 to 12.2 mm. A length of exactly 30 mm still belongs to “over 6 to 30” and gets ±0.2, not ±0.3.
Radii, chamfers and angles
Outside radii and chamfer heights have their own table (GB/T 1804-2000 Table 2), in which classes f and m share one row and c and v another. Angles are looked up by the length of the shorter side (Table 3); for a cone angle, by the length of the cone generatrix. A general angular tolerance controls only the general direction of the lines or line elements of the surfaces, not their form errors.
When a size gets its own tolerance
GB/T 1804-2000 asks for limit deviations to be written after the size when the function needs a tolerance smaller than the general one, or when a larger tolerance is allowed and is cheaper to make. A size between two surfaces made by different processes, for example one cut and one cast, is held to the larger of the two general tolerances.
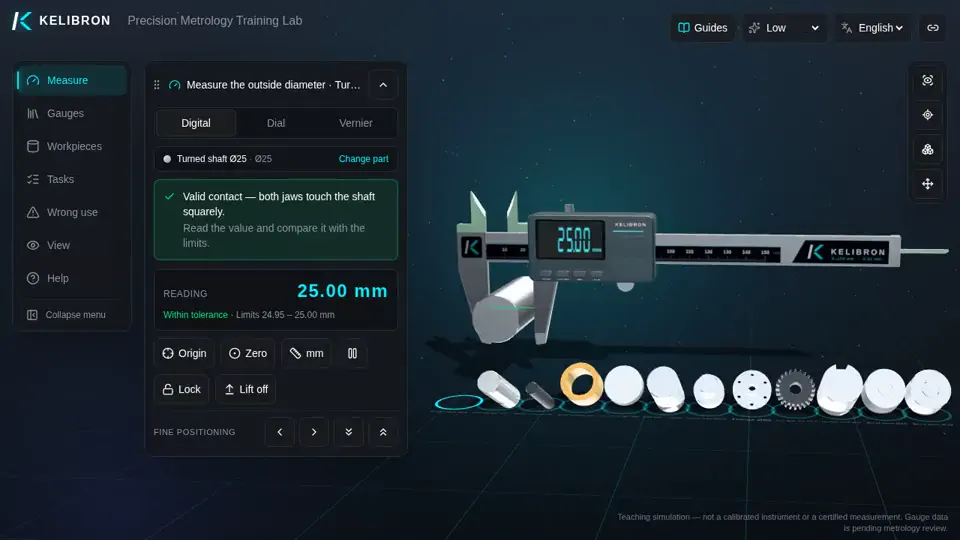
Example: in class m a Ø25 mm diameter would be allowed ±0.2 mm. A shaft drawn as Ø25 0/−0.05 has its own, much smaller tolerance, and only that one applies: 24.95 to 25.00 mm.
Judging a size against a general tolerance
Clause 7 of GB/T 1804-2000 says that, unless otherwise specified, a part that exceeds a general tolerance should not normally be rejected if its function is not impaired. Annex A explains why: the tolerance a function allows is usually larger than the general tolerance, so an occasional excursion rarely harms the part. Only when the function is impaired is the part rejected.
The same annex says that sizes under general tolerances need not normally be inspected when the workshop’s usual accuracy is maintained; the workshop should measure and assess its usual accuracy and check it by sampling. For acceptance by measurement, GB/T 3177-2009 sets the acceptance limits of non-fitting and general-tolerance sizes equal to the limits of size (safety margin A = 0; see acceptance limits).
Example: under GB/T 1804-m a 50 mm length measured at 50.36 mm is 0.06 mm beyond 50.3 mm. Record it as outside the general tolerance; whether the part is rejected depends on its function and on what the contract or drawing says.
Practising in KELIBRON
Every part in the lab carries its own limit deviations, so no lab feature uses a general tolerance; the general tolerance tables are worked on paper. The lab judges by simple acceptance: a value within the closed tolerance interval passes, using the corrected value before it is rounded to the scale. It gives no verdict when the tolerance band is narrower than two divisions of the gauge or when the value lies within half a division of a limit, and an invalid measurement never passes.
In the practice scene a 0.01 mm digital caliper measures the Ø25 0/−0.05 mm shaft, made at 24.98 mm: it passes against its own tolerance, which is the one that applies, not the ±0.2 mm a general tolerance of class m would allow.
References
- GB/T 1804-2000《一般公差 未注公差的线性和角度尺寸的公差》 · 国家质量技术监督局
- ISO 2768-1:1989 — General tolerances — Part 1: Tolerances for linear and angular dimensions without individual tolerance indications · ISO
- GB/T 3177-2009《产品几何技术规范(GPS) 光滑工件尺寸的检验》 · 国家质量监督检验检疫总局、国家标准化管理委员会
How the guides are checked against these sources: About KELIBRON.
Watch it done
Watch in the lab → Follow step by step →
Played back in the lab from domain commands; the reading and verdict come from the measurement model.
Practise in the lab
Questions
What does ISO 2768-m on a drawing mean?
Sizes without their own tolerance take class m (medium) of ISO 2768-1. GB/T 1804-2000 adopts ISO 2768-1:1989 as an equivalent; its Table 1 gives class m ±0.2 mm from over 6 to 30 mm and ±0.3 mm from over 30 to 120 mm.
Is a part outside its general tolerance always rejected?
No. Under GB/T 1804-2000, unless otherwise specified, it should not normally be rejected if its function is not impaired.
Which tolerance applies to a 30 mm length in class m?
±0.2 mm: the range “over 6 to 30” includes 30 mm.
Try it yourself
Open the same setup in the 3D lab and take the reading yourself.
Related guides
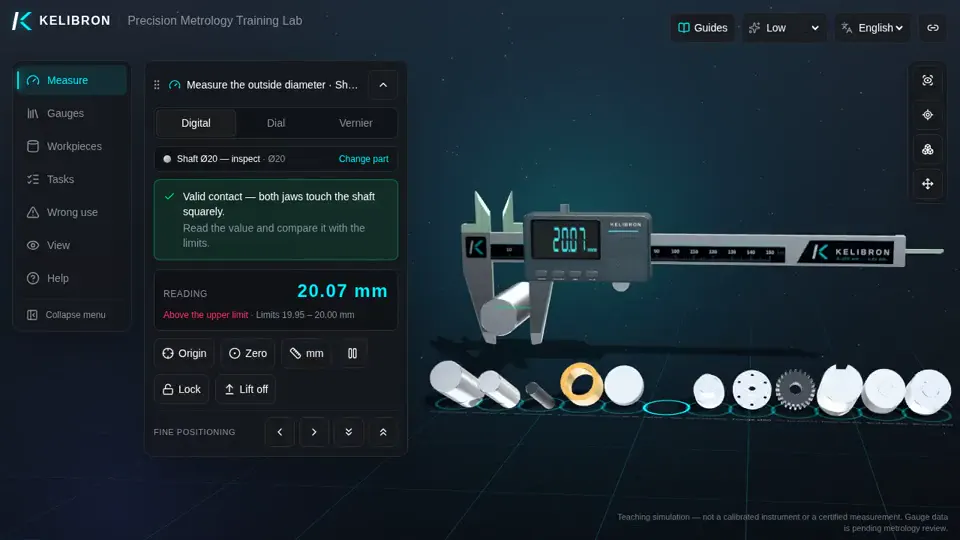 Tolerances and decisionsTolerances and fits basicsA toleranced size gives a nominal size and two deviations.
 Tolerances and decisionsAcceptance limits and the safety margin AUnder GB/T 3177-2009 a plain size is accepted by acceptance limits.
 Tolerances and decisionsCaliper or micrometer? Choosing the instrumentPick an instrument whose accuracy is about one tenth of the tolerance band (the 10:1 rule, a common shop practice; where that is impractical, 4:1 is common and some shops accept 3:1).